PRODUCT INFORMATION
Advanced Manufacturing of ACM Energy Drink
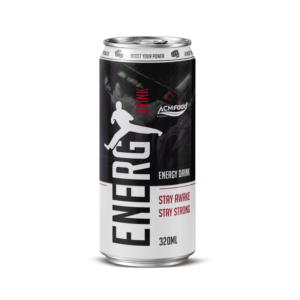
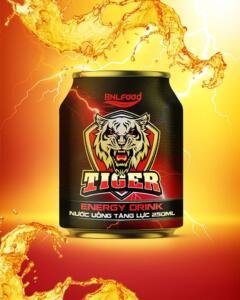
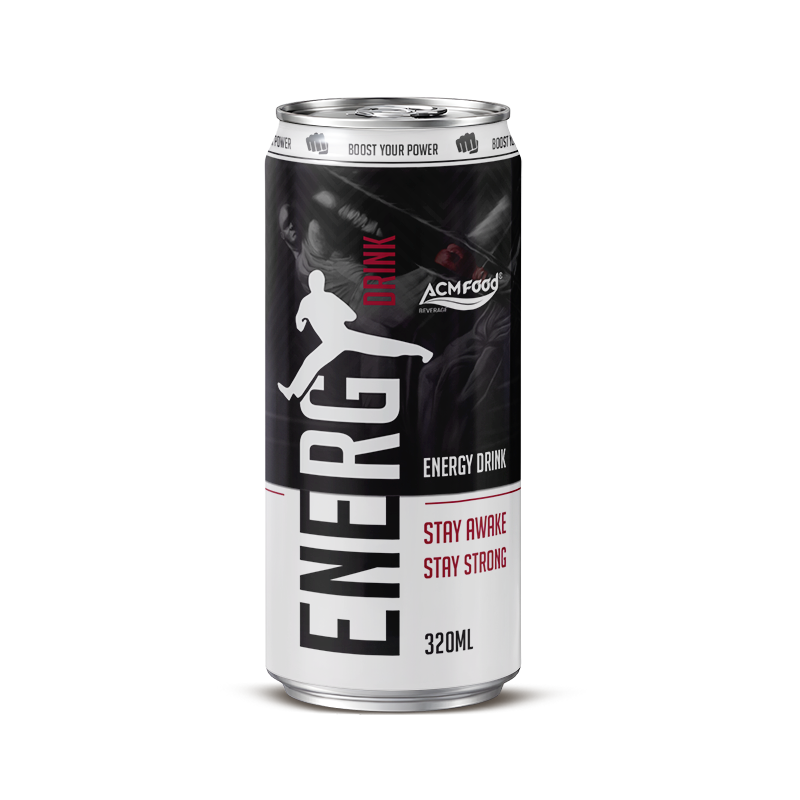
In the competitive landscape of functional beverages, the demand for precision-engineered products continues to rise. ACM Food addresses this need through the industrial-scale production of our signature ACM Energy Drink. Furthermore, we leverage cutting-edge technology to deliver a product that balances taste profile with functional efficacy. Consequently, international buyers recognize our commitment to technical excellence and supply chain reliability. Our facility operates with automated precision, ensuring that every 320ml can meets exact specifications.
Technical Specifications and Formulation
Developing a stable and effective beverage requires rigorous R&D processes. Specifically, the formulation of the ACM Energy Drink undergoes extensive stability testing to ensure ingredient potency throughout its shelf life. Our food scientists optimize the balance of taurine, caffeine, and B-vitamins to maximize consumer satisfaction without compromising safety.
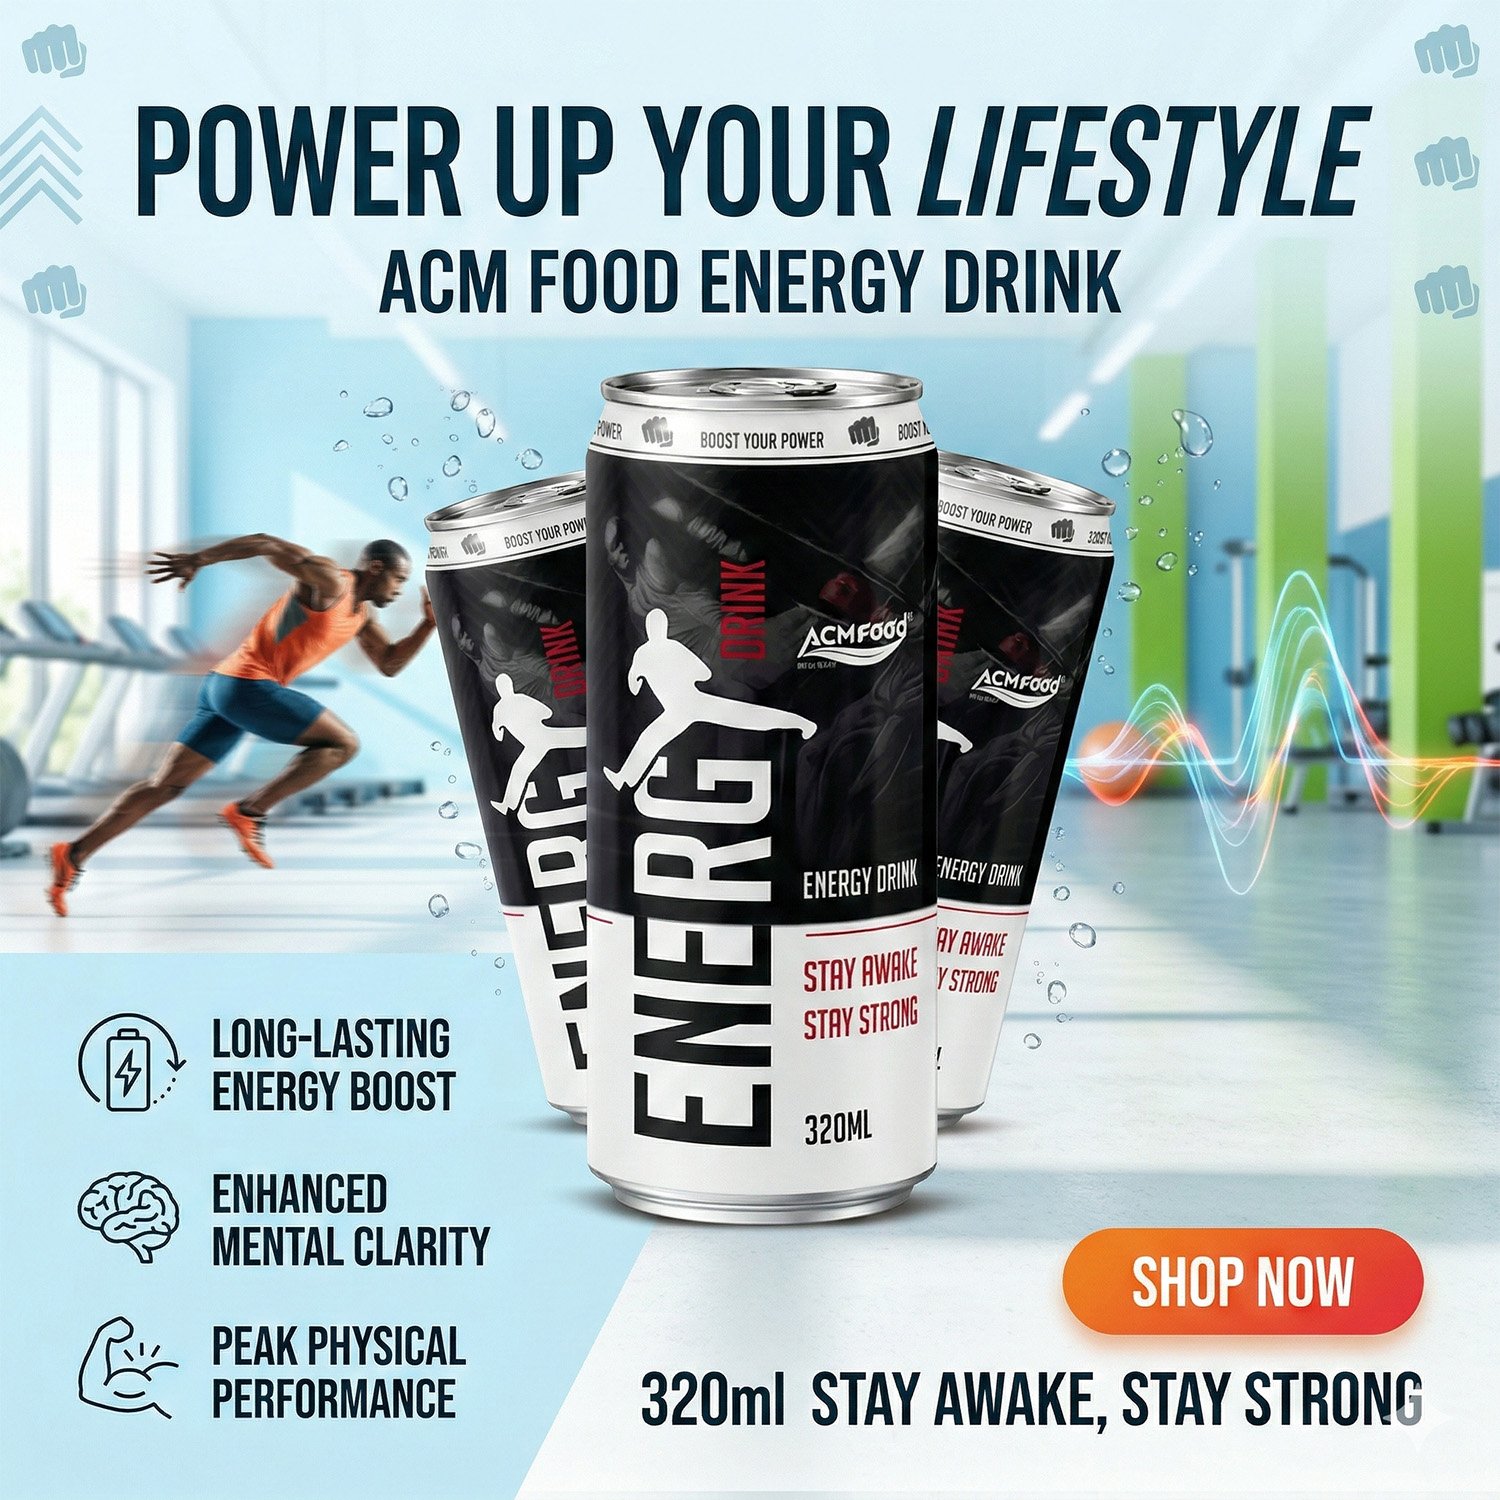
Key technical parameters include:
- Volume: 320ml Slim/Sleek Aluminum Can.
- Carbonation Level: 3.0 – 3.5 volumes of CO2 for optimal mouthfeel.
- Brix Level: Adjusted for regional taste preferences (typically 10-12%).
- Shelf Life: 18 to 24 months under ambient storage conditions.
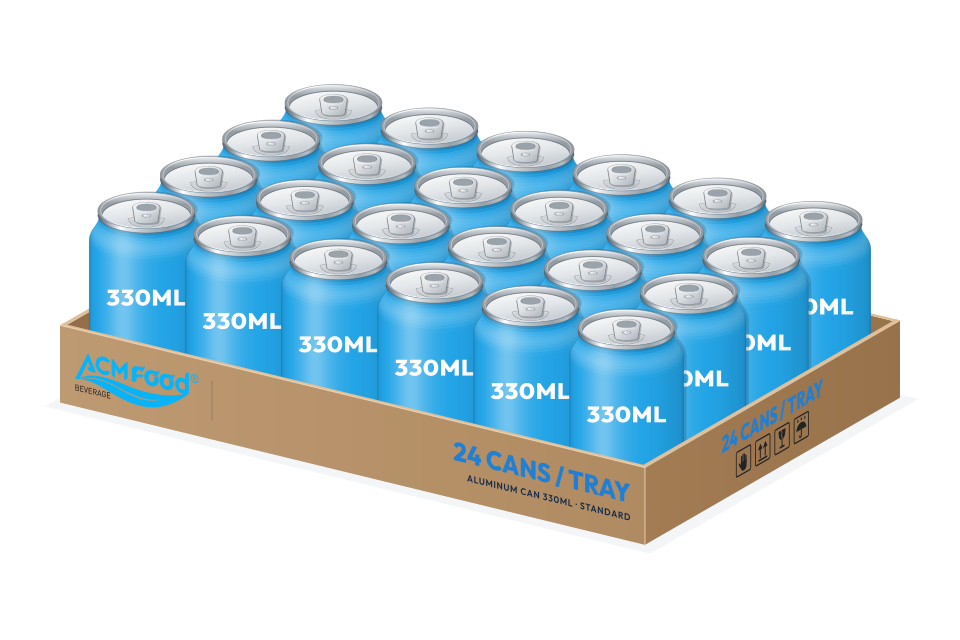
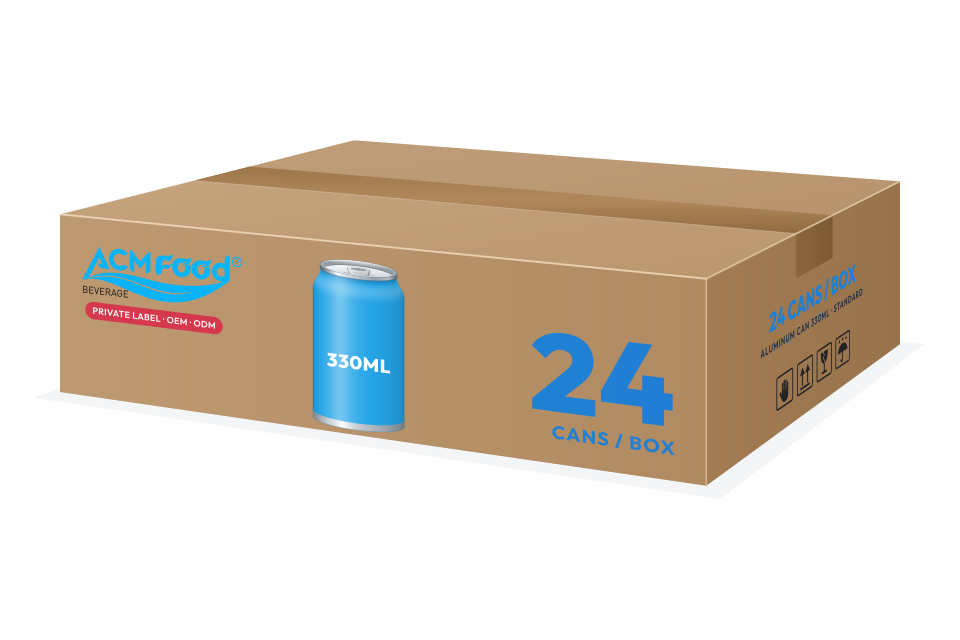
- Packaging: Corrugated trays or shrink-wrap tailored for logistics.
Moreover, we utilize high-grade aluminum sourcing to prevent interaction between the liquid and the liner. This attention to material science ensures the ACM Energy Drink maintains its premium quality from production line to retail shelf.
OEM and ODM Production Capabilities
Beyond our proprietary brand, ACM Food serves as a strategic partner for OEM and ODM projects. We understand that global brands require flexibility. Therefore, our production lines accommodate various formulation adjustments and packaging designs. Whether a client requires a custom flavor profile or a specific nutrient blend, our engineering team executes these requirements with speed.
Additionally, our factory employs high-speed rotary fillers capable of processing thousands of cans per hour. This capacity allows us to fulfill large orders for the ACM Energy Drink or private label equivalents efficiently. Consequently, we minimize lead times for our B2B partners, helping them maintain consistent stock levels in their respective markets.
Quality Control and Compliance
Strict adherence to international standards governs our manufacturing protocols. We do not rely on generic checks; instead, we implement a multi-stage Quality Assurance system. For instance, the seam integrity of every can is monitored using optical inspection systems to prevent leakage and spoilage. This ensures the ACM Energy Drink remains safe and carbonated during long-distance transport.
Furthermore, our facility maintains compliance with major global safety certifications. By strictly following HACCP and ISO protocols, we guarantee a contaminant-free environment. B2B buyers can confidently import our products, knowing they meet the stringent regulatory frameworks of major export destinations. Ultimately, ACM Food delivers a technically superior product designed for scalable business growth.