
Premium Milk Coffee Beverage Experience
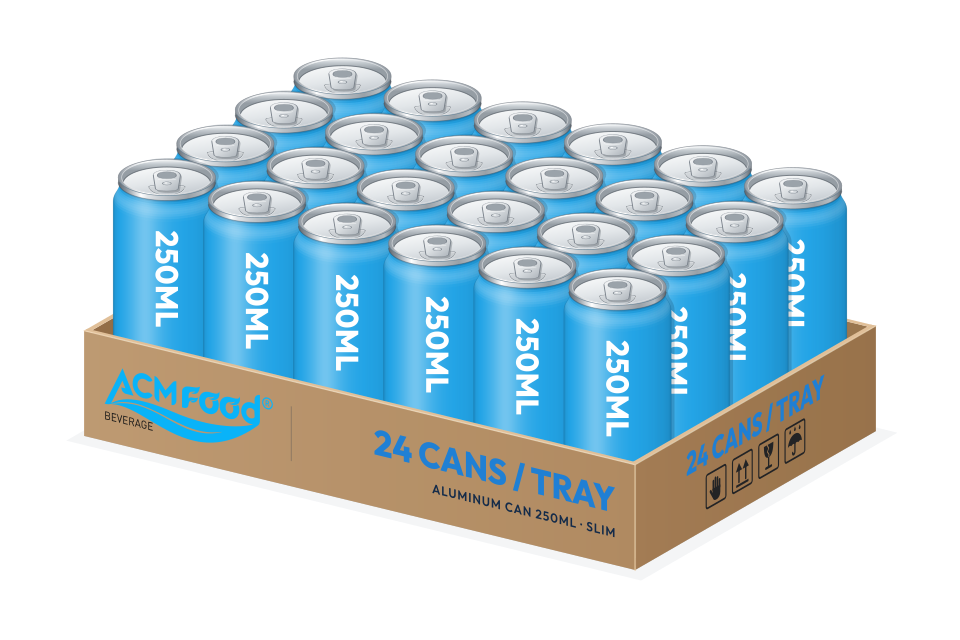
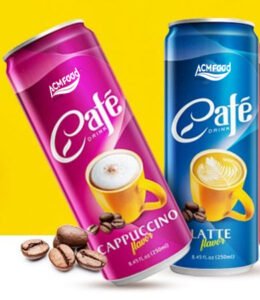
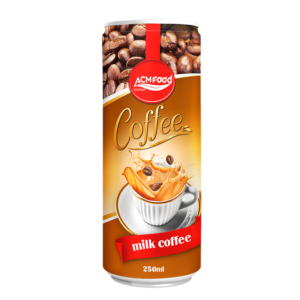
The ready-to-drink milk coffee 250ml delivers sophisticated fusion of premium Arabica coffee and creamy milk in convenient aluminum packaging. This expertly crafted beverage combines rich coffee aroma with smooth milk texture, creating balanced flavor appealing to coffee enthusiasts and casual consumers. The 250ml can ensures freshness and portability for on-the-go consumption while maintaining quality through advanced packaging technology.
Manufactured at ACM Beverage’s advanced facilities, this milk coffee undergoes rigorous quality control for consistency and excellence. The recipe achieves optimal harmony between coffee intensity and milk creaminess, eliminating excessive bitterness while preserving authentic coffee character. This results in premium ready-to-drink option meeting modern consumer demands for convenience without compromising taste or quality standards in competitive markets.
Natural Milk Coffee Ingredients Composition
Featuring premium Arabica coffee beans from sustainable farms and standardized milk for consistent creaminess, this formulation includes natural sweeteners and food-grade stabilizers. The ingredient profile emphasizes recognizable, quality components while avoiding artificial additives. This approach creates exceptional taste while aligning with consumer preferences for natural coffee beverages with transparent ingredient declarations.
The complete formulation incorporates carefully roasted coffee extract delivering optimal aroma, milk processed for texture consistency, natural sweeteners complementing core flavors, stabilization systems maintaining homogeneity, and purified water ensuring clean taste. This philosophy supports both sensory enjoyment and consumer trust through quality-focused ingredient selection and processing methodologies across production cycles.
Functional Milk Coffee Benefits
This balanced beverage provides moderate caffeine (80-100mg per serving) for gentle energy support alongside milk’s nutritional value including calcium and protein. The formulation optimizes digestibility by buffering coffee’s natural acidity with milk components. Key benefits include convenient energy sourcing for daily routines, nutritional contribution supporting dietary requirements, hydration through beverage format, mood enhancement via comforting sensory experience, and social compatibility across various settings.
The integrated approach ensures broad demographic appeal while addressing multiple consumption occasions. The milk-coffee synergy creates beverage suitable for consumers who appreciate coffee but may experience discomfort with traditional preparations, offering digestible alternative without sacrificing coffee enjoyment or functional benefits derived from moderate caffeine and milk nutrients supporting daily wellness.
Market-Ready Coffee Drink Applications
The 250ml ACM Milk Coffee Drink suits diverse distribution channels including retail stores, food service venues, corporate settings, educational institutions, and travel locations. Its shelf-stable packaging and consistent quality make it ideal for convenience stores, supermarkets, cafes, restaurants, office pantries, campuses, airports, and vending operations. The product bridges traditional canned coffee drinks and premium specialty beverages, offering superior quality with convenience driving repeat purchase behavior.
For businesses expanding milk-based beverage portfolios, this product attracts both existing coffee consumers and new market entrants. Addressing growing demand for convenient coffee solutions and increasing quality expectations, it appeals to professionals, students, travelers, and anyone seeking quality coffee without preparation requirements. The versatile positioning supports multiple market applications while delivering consistent consumer satisfaction across various consumption scenarios and demographic segments in competitive beverage marketplace with evolving preferences.
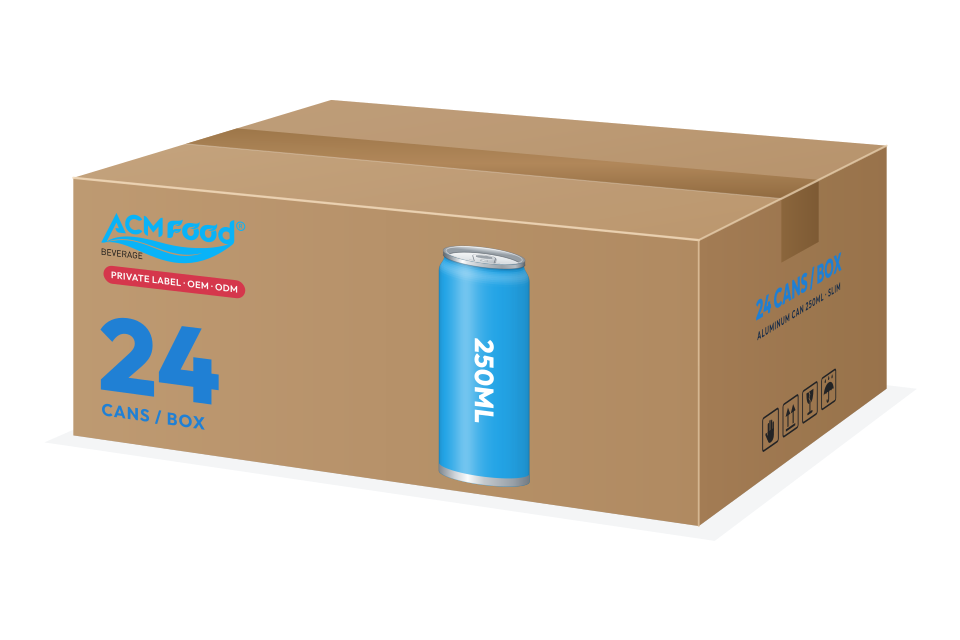
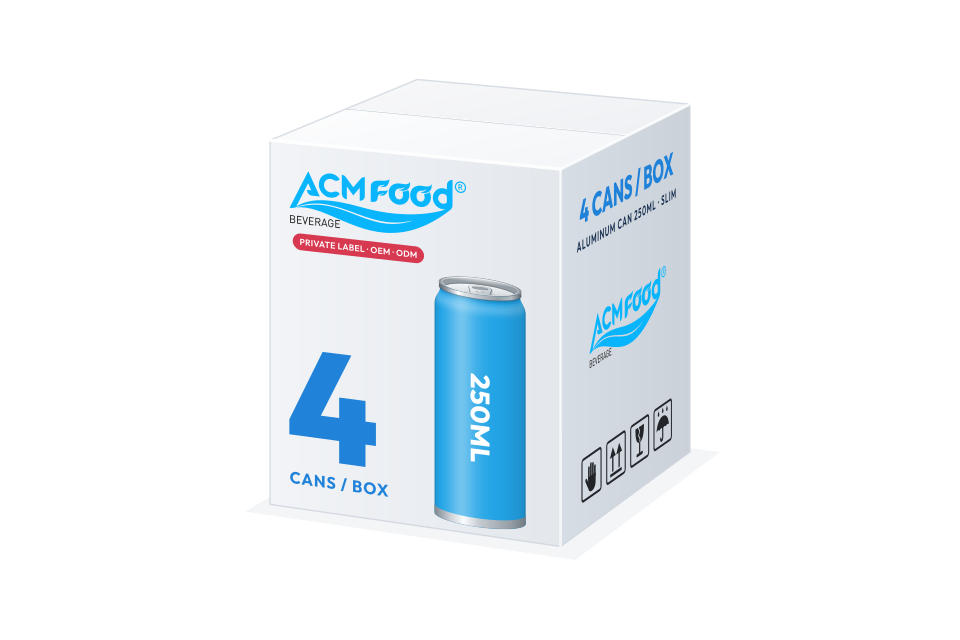
The product’s development considered contemporary consumption patterns including busy lifestyles, increasing mobility, and demand for premium convenience. Packaging design facilitates easy handling, storage, and disposal while maintaining visual appeal on retail shelves. Quality assurance protocols ensure every unit meets established standards for taste, safety, and consistency, building brand reputation and consumer confidence through reliable performance across distribution networks and usage contexts.